


Introduction
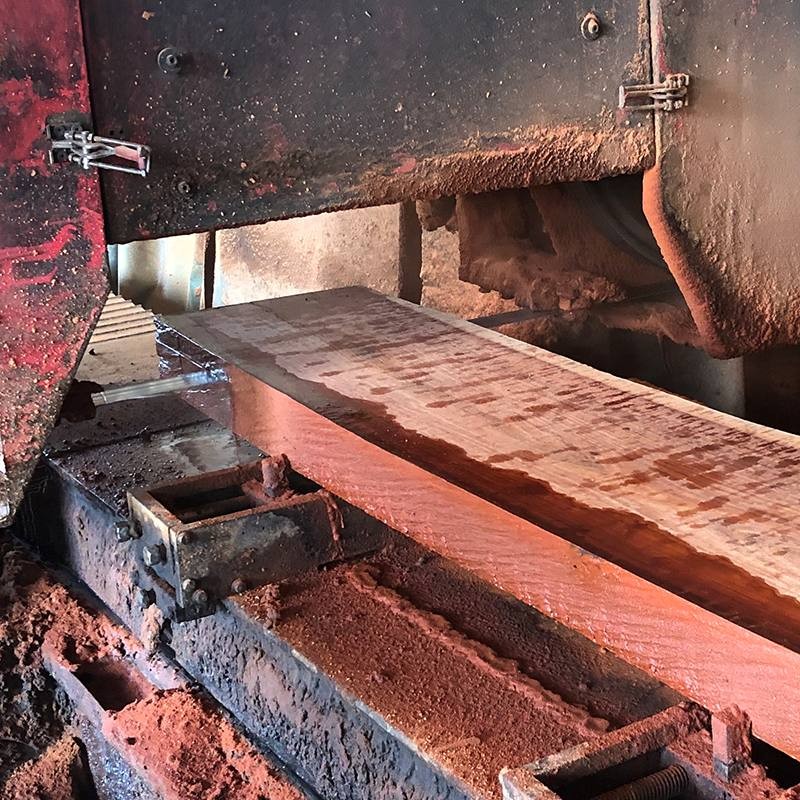
Engineered specifically for secondary panel processing facilities, cabinet manufacturers, and large-scale industrial distributors, our Plywood Band Saw Blade addresses the unique challenges of cutting composite wood materials. Plywood panels feature alternating grain orientations and abrasive adhesive layers that accelerate conventional tool wear, often causing edge chipping and laminate tear-out. Produced at our specialized manufacturing facility in Zhejiang, China, Sipu utilizes high-alloy European steel substrates and precision-ground tooth geometries to deliver clean, splinter-free cuts across multi-layered hardwood and softwood panels. Global B2B procurement professionals rely on our blades to maximize sheet yield and reduce secondary edge-finishing costs in continuous production lines.
Specification
| Parameter | Available Configuration |
|---|---|
| Product Type | Bandsaw blade for plywood and engineered wood |
| Primary Materials | Plywood, veneered panels, MDF and selected wood-based boards |
| Blade Material | Carbon steel / alloy steel according to application |
| Blade Width | Customized |
| Blade Thickness | Customized |
| Tooth Pitch | Multiple TPI options |
| Tooth Profile | Regular, variable pitch, hook and application-specific profiles |
| Tooth Set | Customized according to material and cutting requirement |
| Loop Length | Customized to machine |
| Welding | Endless welded loop available |
| Packaging | Standard industrial or OEM/private-label packaging |
| Supply Type | Bulk, wholesale and OEM/ODM |
Core Advantages
To ensure complete technical transparency for industrial procurement teams, the structural performance of every Plywood Band Saw Blade is backed by specific metallurgical and mechanical design principles:
Zero-Degree Rake Angle Precision
Unlike aggressive log-cutting saws, our panel blades utilize neutral or low-positive rake angles (0° to 5°) to scrape rather than gouge composite layers, preventing catastrophic delamination of interior glue lines.
Alternating Bevel (ATB) Tooth Geometry
Precision-ground alternate top bevel patterns create a shearing action from both sides of the kerf, severing glue bonds and wood fibers cleanly without thermal burning.
Controlled Hardness Differential
Tooth tips are induction-hardened to 62–64 HRC for maximum abrasion resistance, while the backing strip retains a flexible 42–44 HRC structure to withstand high continuous flexing on narrow band wheels.
Optimized Gullet Mirror Finish
Inter-tooth gullets undergo automated vibratory polishing to eliminate microscopic ridges, preventing resin buildup and sawdust packing when cutting moisture-resistant exterior glues.
Tooth Selection for Plywood Processing
The correct tooth pitch is determined mainly by panel thickness and the amount of material each tooth needs to remove.
A blade with an excessively coarse pitch can produce a more aggressive cut than necessary on thin plywood. A blade with teeth that are too fine for a thick panel may have insufficient gullet space for efficient waste removal.
Fine Tooth Configuration
More teeth engaged in the material can help distribute the cutting load across a larger number of teeth. This can be useful for thinner plywood, veneered boards, and applications where edge appearance matters.
Coarser Tooth Configuration
A more open tooth arrangement provides greater gullet volume for sawdust and chips. This becomes more relevant when cutting thicker panels or when the feed rate generates a larger chip load.
Regular Tooth Profile
A regular tooth arrangement can provide a balanced solution for general plywood processing where the priority is predictable cutting rather than aggressive material removal.
Variable Pitch
Variable pitch can be considered where vibration control is important. The changing tooth spacing can help avoid a single repetitive cutting frequency becoming dominant during continuous cutting.
Packing
About Us

Our Certificate


FAQ
Q: What is the minimum order quantity (MOQ) for custom-welded loops of the Plywood Band Saw Blade?
A: For standard stock dimensions, our MOQ begins at 50 welded loops or equivalent coil lengths to facilitate sample testing for new distribution partners. Customized tooth configurations or private-label box designs are evaluated based on total running meters per production batch.
Q: How are blades protected against oxidation during maritime transit?
A: Each blade loop is coated with a specialized rust-inhibiting industrial compound, wrapped individually in heavy-duty VCI (Volatile Corrosion Inhibiting) paper, secured inside corrugated sleeves, and packed into sturdy, fumigation-free wooden crates designed for long-term ocean shipping.
Q: What feed rate adjustments are recommended when transitioning from soft plywood cores to dense hardwood particle boards?
A: Operators should reduce standard feed rates by 15% when encountering high-density particle board or phenolic resin cores to prevent localized thermal overloading and maintain clean, burn-free edge finishes.
Q: Can your engineering team configure specialized tooth sets for abrasive fire-retardant panel boards?
A: Yes. Our application engineers analyze board chemical composition, resin density, and machine horsepower to recommend customized carbide or high-alloy tooth treatments optimized for abrasive specialty panels.
Hot Tags: plywood band saw blade, China plywood band saw blade manufacturers, suppliers, factory, bandsaw blade for edge trimming, bandsaw blade for furniture panels, Carbide Tooth Bandsaw Blade, skip tooth wood bandsaw blade, wide wood bandsaw blade, wood bandsaw blade


