



Product Introduction
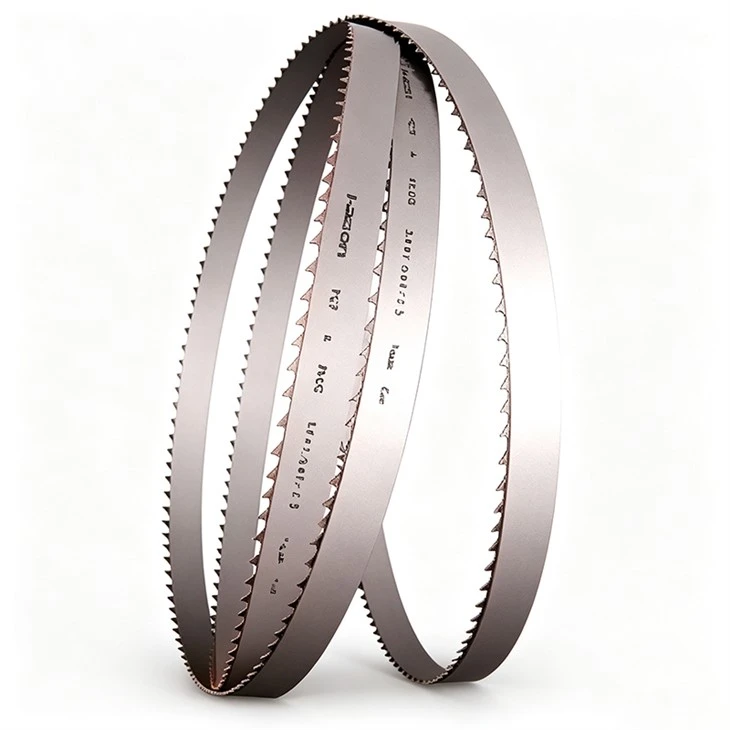
This blade runs where the saw doesn't stop: multi-shift stainless tubing cells, bundled structural cutting, and bar stock sawing on automatic machines. The cutting edge is M42 or M51 high-speed steel; the backing strip is a low-alloy spring steel selected for fatigue resistance under repeated bending over the wheels. Widths from 13 mm to 67 mm cover the common production saw sizes, and every loop is welded to the length your machine actually runs-no shimming, no reworking the guides on arrival.
Tooth edge and backing strip
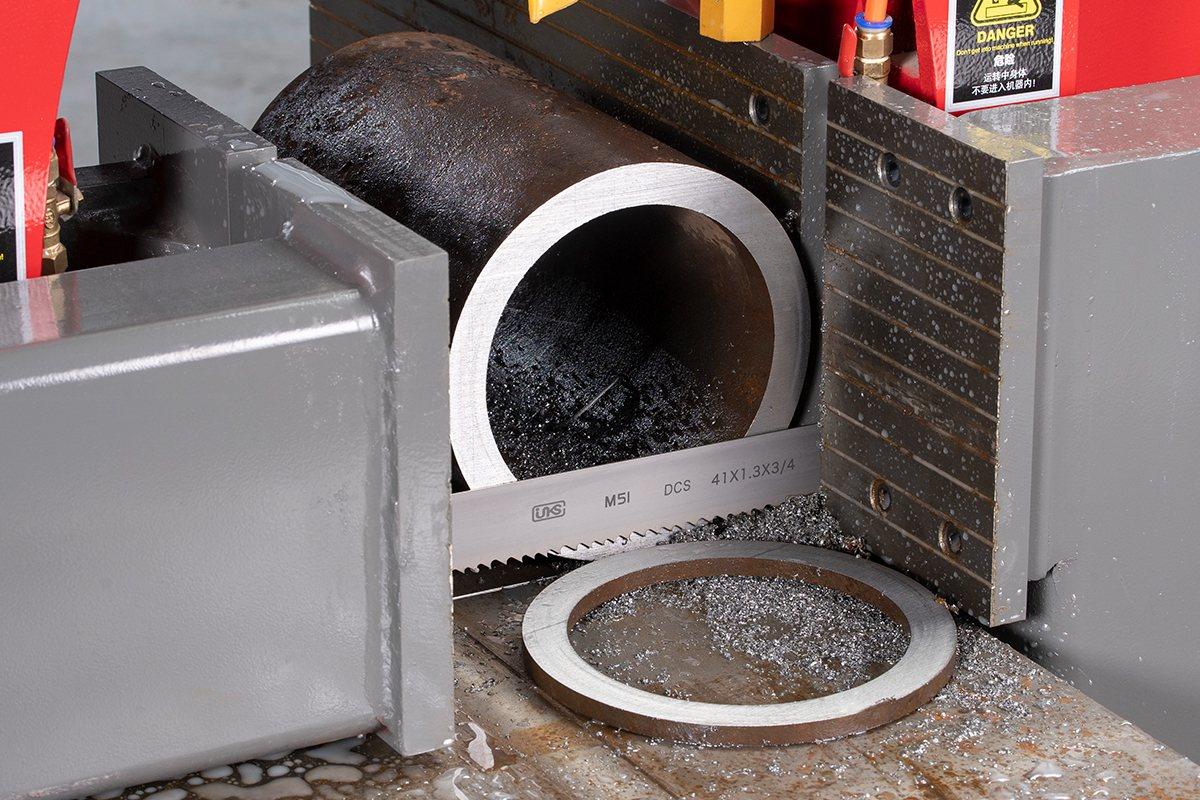
M42 tooth tips are cobalt-alloyed HSS. Hardness sits at HRC 67–69. That edge holds up in tool steel, 304/316 stainless, and alloy bar up to roughly 45 HRC. M51 runs a higher cobalt and vanadium content in the tooth alloy; tip hardness reaches HRC 68–70, and the working ceiling moves to about 50 HRC. The practical difference shows up on continuous stainless and nickel-based work: M42 cuts clean but dulls faster when the machine runs the same stainless tube every shift; M51 absorbs that duty without the same edge breakdown.
The backing strip is not generic carbon steel. We use a low-alloy spring grade such as 46CrNiMoVA. It flexes repeatedly without taking a permanent set and resists the cracking that starts at the back edge when tension runs high on a production saw.
Weld and heat treatment
A production blade fails at the weld or it doesn't fail at all. We weld with a CNC-controlled process and hold weld-joint flatness deviation to 0.02 mm or less. After welding, the joint passes through a controlled annealing step matched to the backing temper. That matters because an untempered weld is hard but brittle; a correctly annealed weld bends with the band instead of cracking beside it.
Each production batch is checked with an image measuring instrument for weld alignment and tooth spacing. Records stay with the batch number, so a distributor can trace a performance question back to the weld cell and the steel lot.
Variable pitch, chosen against the cut section
Constant pitch is not offered for production cutting on mixed sections. The standard tooth sequences are 2/3, 3/4, 4/6, 5/8, and 0.75/1.25, plus finer variable pitches such as 8/12 and 10/14 for thin-wall tube. The pitch is selected against the contact length through the cut: a solid bar takes a coarser pitch for chip clearance; a bundled tube section or an I-beam flange that changes thickness in one pass needs a variable pitch to keep the tooth load from spiking at the transition. The variable sequence breaks the harmonic that a constant pitch sets up, which is why the blade runs quieter and the tooth corners stop chipping on structural work.
What the blade is asked to cut
The common production materials are 304/316 stainless, Cr12MoV-type die steel, 4140/4340 alloy bar, 6061/7075 aluminum, titanium, thick-wall tube, and bundled structural. It is not a wood blade and not a meat blade; the tooth geometry and backing tension are set for metallic chip formation and the feed pressures of a metal saw.
Ordering, lengths, and marking
Widths run 13, 16, 19, 27, 34, 41, 54, and 67 mm. Length is welded to your machine spec. If you stock coils for your own welder, we supply bulk coil; if you sell to end users, we ship finished loops. MOQ starts at 10 blades for welded loops. Standard widths leave the warehouse within 48 hours; bulk and custom lengths run 7–14 working days. For distributors, laser marking with your brand, part number, and tooth spec is available on bulk orders-no additional tooling charge for standard layouts.
| Width (mm) | Tooth pitch (TPI) | Tooth material | Backing strip | Typical production cut |
| 13 / 16 / 19 | 4/6, 5/8, 8/12 | M42 or M51 | 46CrNiMoVA | Thin-wall tube, small solids, bundle cutting |
| 27 / 34 / 41 | 2/3, 3/4, 4/6 | M42 or M51 | 46CrNiMoVA | Structural, medium solids, stainless tube |
| 54 / 67 | 1.4/2, 2/3, 0.75/1.25 | M51 | 46CrNiMoVA | Large bar, heavy section, high-volume stainless |
FAQ
Q: How do we decide between M42 and M51 for a customer's production saw?
A: Look at the cut list, not the blade price. If the saw runs mixed mild steel, aluminum, and occasional stainless under 45 HRC, M42 covers it. If the machine cuts stainless or nickel alloy every shift, M51's higher alloy content at the tooth tip holds hardness longer and reduces mid-shift changes. A blade that dulls two hours early costs more in downtime than the price gap between the two grades.
Q: What weld documentation comes with a production order?
A: Weld flatness is held to 0.02 mm and checked with an image measuring instrument. Batch records link the finished loop to the weld cell and steel lot. If a weld fails before the teeth dull under normal feed and speed, we replace the blade.
Q: Do you supply coils as well as welded loops?
A: Both. Distributors with a welder take bulk coil; distributors selling to end users take finished loops cut to the machine length. Coil and loop pricing are quoted separately so you can compare against your own welding cost.
Q: What break-in do you recommend for a new production blade?
A: Run the first 20 minutes at 50% of the normal feed rate with the recommended band speed. This dresses the ultra-sharp tooth edge and prevents micro-chipping at the corners. A controlled break-in typically adds 25–50% to usable blade life on production saws.
Q: Can we combine multiple widths and tooth pitches in one shipment?
A: Yes. Mixed-width and mixed-pitch orders ship on the same pallet as long as each item meets the 10-blade MOQ. Standard widths ship within 48 hours; custom welded lengths add 7–14 working days.
Hot Tags: production cutting bandsaw blade, China production cutting bandsaw blade manufacturers, suppliers, factory, heavy duty bandsaw blade, Hss Bandsaw, M42 Metal Bandsaw, metal bandsaw blade for thin sheets, metal cutting bandsaw blade for nickel, skip tooth metal bandsaw blade


